
The Preferred Engineering Cavity Seal System provides nuclear facilities with a practical solution for sealing the reactor annulus while simplifying installation and verification. The system uses segmented EPDM extrusions that are custom-made to fit your reactor annulus. Polished stainless-steel cover plates work with stainless-steel J-bolts and cam-actuated toggle nuts to compress each seal securely. Unlike systems that depend […]
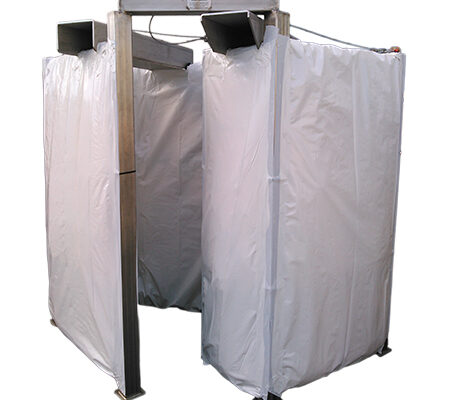
Place ALARA Shielding Right Where You Need It
Preferred Engineering’s custom designed products are built, originally, for the needs of a specific customer. However, once they are designed, our customers find them useful in many other situations for many other nuclear facilities. One great example is the Portable Cavity Shield Frame, which was initially designed for a customer who needed to create an ALARA zone inside […]

Fuel Storage Warning Signs You Should Not Ignore
A fuel oil system is only as reliable as the condition of the fuel inside it. For facilities that depend on backup generation or continuous fuel supply, catching problems early is the difference between a maintenance call and an emergency. Here are four warning signs that your fuel storage system needs attention: Water in fuel samplesWater intrusion is […]
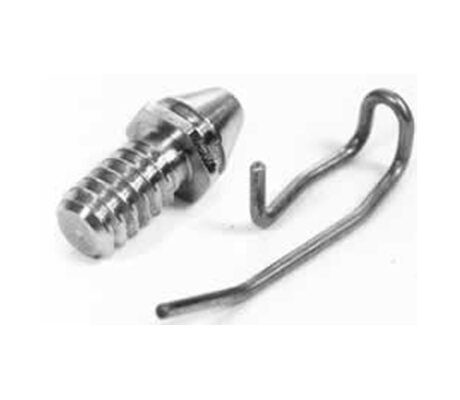
How to Make Your RPV O-Ring Installation Easier
When every second counts, tools that speed up the job make all the difference. That’s the case with the RPV O-Ring Clips and Installation Tools. The RPV O-Ring Clips and Installation Tools speed up installation of the RPV O-rings into the RPV head. This not only saves time during tight outage schedules but reduces radiation exposure time for nuclear technicians. […]

Outstanding Safety in a Lightweight Package
What can you do when you need a safety railing where there isn’t one built into your nuclear facility? It’s not always the best option (or even possible) to attach a permanent structure. That’s where Preferred Engineering’s Lightweight Railings come in. We know that OSHA standards require a standard of safety, but even more than standards, we want […]

Today’s Boiler: Visibility and Control in the Boiler Room
SCADA Systems: The Backbone of Modern Boiler Room Operations Managing a modern boiler room means juggling burners, fuel systems, feedwater equipment, pumps, valves, and instrumentation all at once, all in real time. One missed signal can mean downtime, safety risks, or worse. So how do today’s operators stay ahead of it all? The answer is SCADA. Supervisory Control […]

Measuring the Flow of Progress: Then and Now
Before microprocessors and digital control systems dominated boiler rooms, industrial automation relied on precise analog instruments like those pictured below from Republic Instruments and Controls of Chicago. Their line of mercury U-tube electrical flow meters, pressure/llevel gauges, CO₂ analyzers, and boiler meters helped operators monitor everything from steam and air flows to combustion efficiency, all without today’s electronics. […]

Rethinking fuel control
As seen in Data Centre and Network News Distributed architecture for resilient infrastructure Uninterrupted power is non-negotiable for data centres to provide continuity through every possible scenario, from extreme weather events to grid instability in an ageing infrastructure. Generators, of course, are central to this resilience, but we must also consider the fuel storage infrastructure that powers them. […]

Advancing Low NOx Combustion with Natural Gas & Biogas Piping Trains
Preferred recently completed a Natural Gas and Biogas Piping Train, designed and manufactured in-house, and paired with our API Ranger Burner. This system is built to meet the highest performance and environmental standards, featuring: ✔ Ultra Low NOx emissions for regulatory compliance and environmental responsibility✔ 10:1 turndown capability on both natural gas and biogas for precise load control […]

Combustion Solutions for Ultra-Low NOx — A Custom Application
At Preferred Utilities, Combustion Crew continues to deliver advanced combustion solutions tailored for specialty and industrial applications. Recently, a customer approached us with a challenge: their SCR (Selective Catalytic Reduction) system required flue gas temperatures of 700°F to function effectively, but their Thermal Oxidizer was only producing 200°F. Without proper temperature elevation, the ammonia injection process would not […]