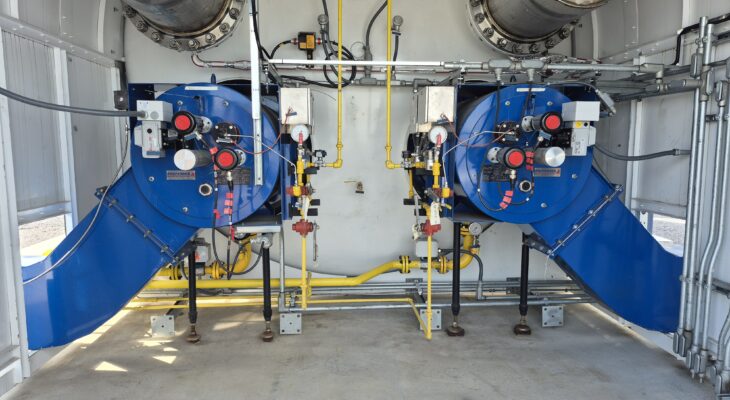
Preferred recently completed a combustion and controls package for a cryogenic facility in Canada. The scope covered burners, burner management and combustion controls, power distribution, and fuel gas piping for a dual-chamber water bath heater, all designed, built, and supplied by Preferred as a single integrated system. Project at a glance Burners and heater configuration Water bath heaters […]
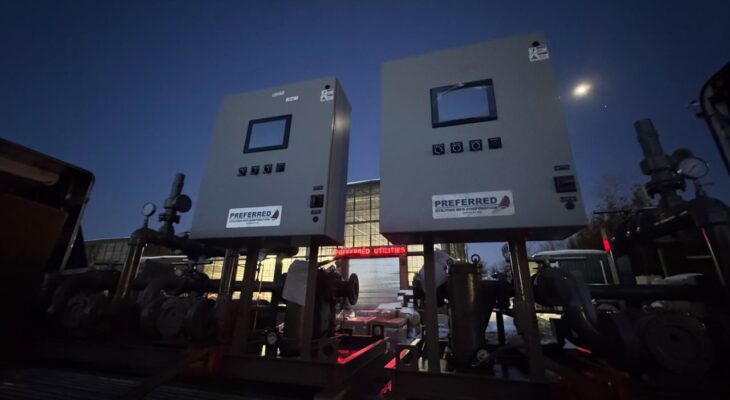
Answering the Call: Morning, Noon or Night
Another round of equipment just left our facility in Danbury, CT: pump skids, day tanks, flow control manifolds, jockey skids, and filtration skids, all headed to yet another data center client. It’s become a familiar sight on our shipping floor, and there’s a good reason for that. Data centers don’t get to have a bad day. When a […]

Making Waste-to-Energy Plants More Reliable With Burner Retrofits
As seen in POWER Magazine Inconsistent fuel quality puts constant strain on aging waste-to-energy boiler systems. Modernizing startup burners, combustion controls, and flame detection can restore reliability and keep plants code-compliant—without the cost of a full replacement. Waste-to-energy (WTE) infrastructure turns municipal garbage into usable power. In theory, the process is efficient, reliable, and sustainable. Unfortunately, the reality […]

Growth and Sustainability With Ultra-Low & Nano-NOx Burners
Environmental regulations continue to evolve and tighten around NOx emissions. In parts of Northeast and Southern California, sub-9 ppm NOx combustion for natural gas has already become the practical standard, while states like Maryland have proposed phased adoption of near-zero-NOx systems for institutional boilers by 2029. A facility’s emissions profile now directly influences whether it can renew operating […]

Today’s Boiler: Visibility and Control in the Boiler Room
SCADA Systems: The Backbone of Modern Boiler Room Operations Managing a modern boiler room means juggling burners, fuel systems, feedwater equipment, pumps, valves, and instrumentation all at once, all in real time. One missed signal can mean downtime, safety risks, or worse. So how do today’s operators stay ahead of it all? The answer is SCADA. Supervisory Control […]

SCADA Deployment for a Mission Critical Facility — Ahead of Schedule
Mission critical infrastructure depends on reliable fuel oil handling where there is no margin for error, and no room for delays. That’s why we’re pleased to share that Stage 2 of an ongoing large-scale deployment for a mission critical facility has been successfully completed, and it came in ahead of schedule. Project Background A year ago, Preferred was […]

SCADA Integration for a New York Hospital: Reliable, Connected, and Built to Last
Our latest SCADA deployment for a major New York hospital is a testament to our commitment to excellence and delivering solutions – a fully integrated system designed to keep mission-critical operations running safely, efficiently, and with complete visibility. Project Overview The system was engineered to monitor and control four boilers and one feedwater center, pulling and integrating data […]

10 Years of Energy Savings from One Smart Investment
When it comes to boiler room efficiency, even a small upgrade can lead to major, long-term savings. That’s what happened at a central plant in Maryland, where a simple retrofit led to over a decade of energy and cost reductions. The project started with the facility installing a Variable Frequency Drive (VFD) on an aging linkage boiler, paired […]

Dual-Fuel Flexibility and Performance
With Preferred’s SPEC COM Burners and fuel blending technology. Preferred’s Combusion crew continues to push the boundaries of performance and flexibility in industrial combustion systems. A recent project involved outfitting two (2) Superior 1400 HP firetube boilers with Preferred’s advanced low NOx SPEC COM burners and gas blending skids. Each boiler is rated for approximately 48,300 lb/hr of […]

Combustion Solutions for Ultra-Low NOx — A Custom Application
At Preferred Utilities, Combustion Crew continues to deliver advanced combustion solutions tailored for specialty and industrial applications. Recently, a customer approached us with a challenge: their SCR (Selective Catalytic Reduction) system required flue gas temperatures of 700°F to function effectively, but their Thermal Oxidizer was only producing 200°F. Without proper temperature elevation, the ammonia injection process would not […]